
螺纹盖注塑模具设计(含CAD零件装配图,UG三维图)
螺纹盖注塑模具设计(含CAD零件装配图,UG三维图)(论文说明书14000字,CAD图11张,UG三维图,模流)
摘要
伴随着经济水平的不断提高和社会的不断发展,也推动了机械工业的进步。从而随着人们生活水平的不断提高,日常生活中使用的塑料产品各种各样。本文主要围绕端盖进行注塑模具设计,通过塑料成型的技术来生产加工,设计出一套高效经济的模具结构。
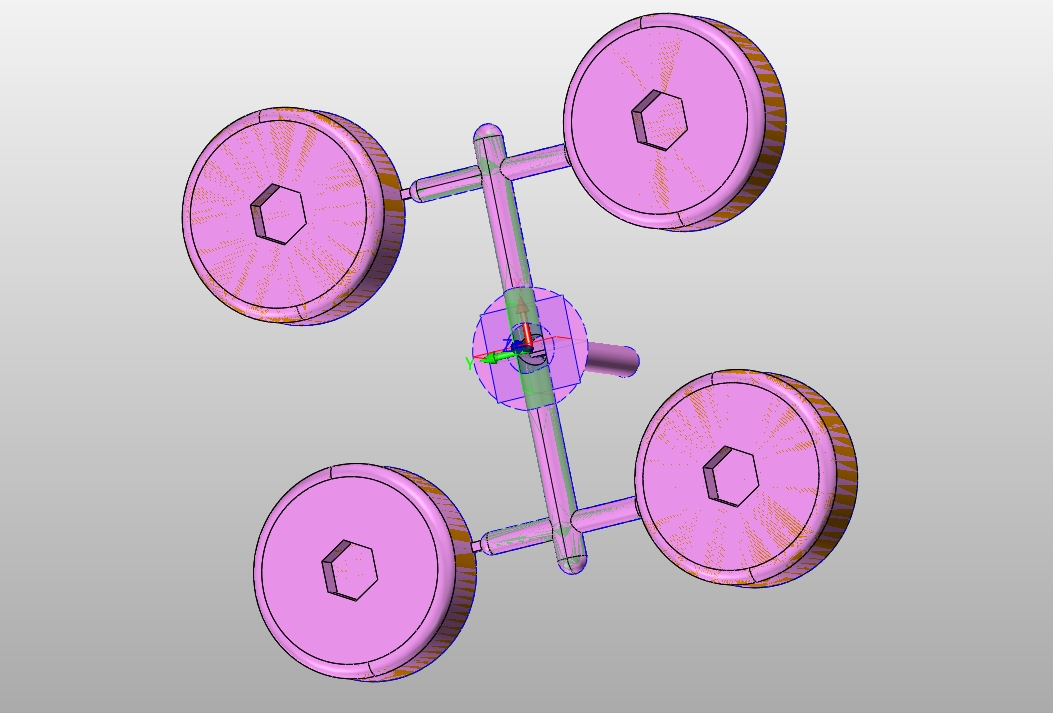
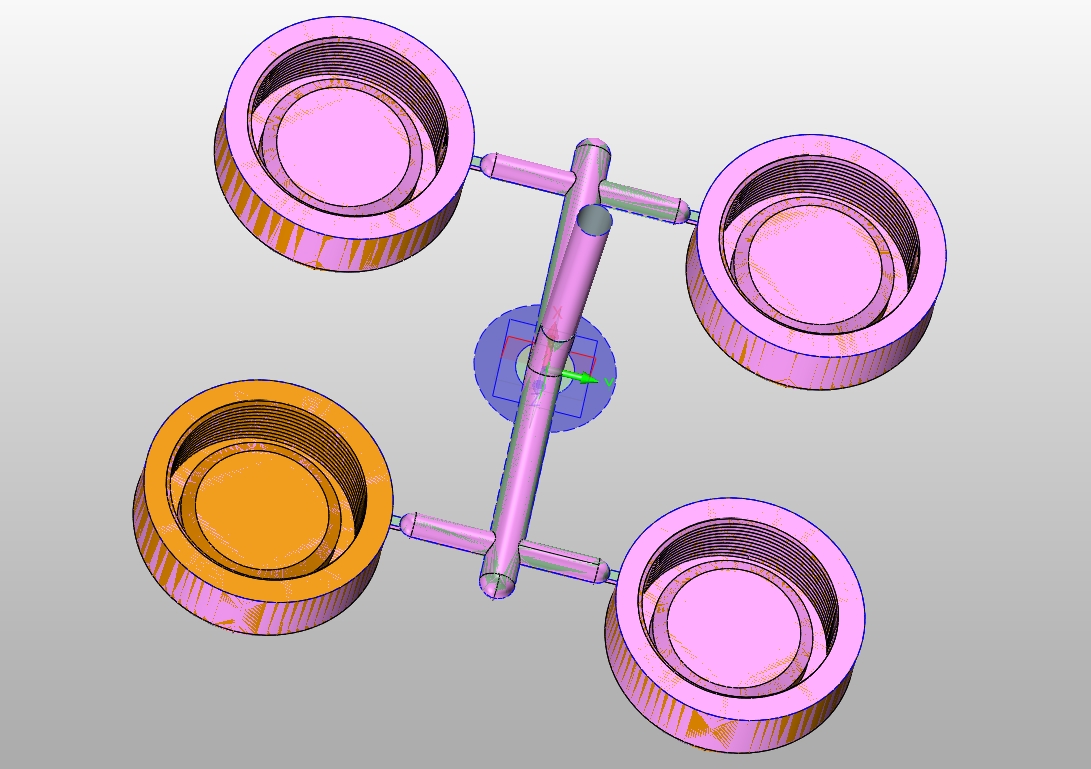
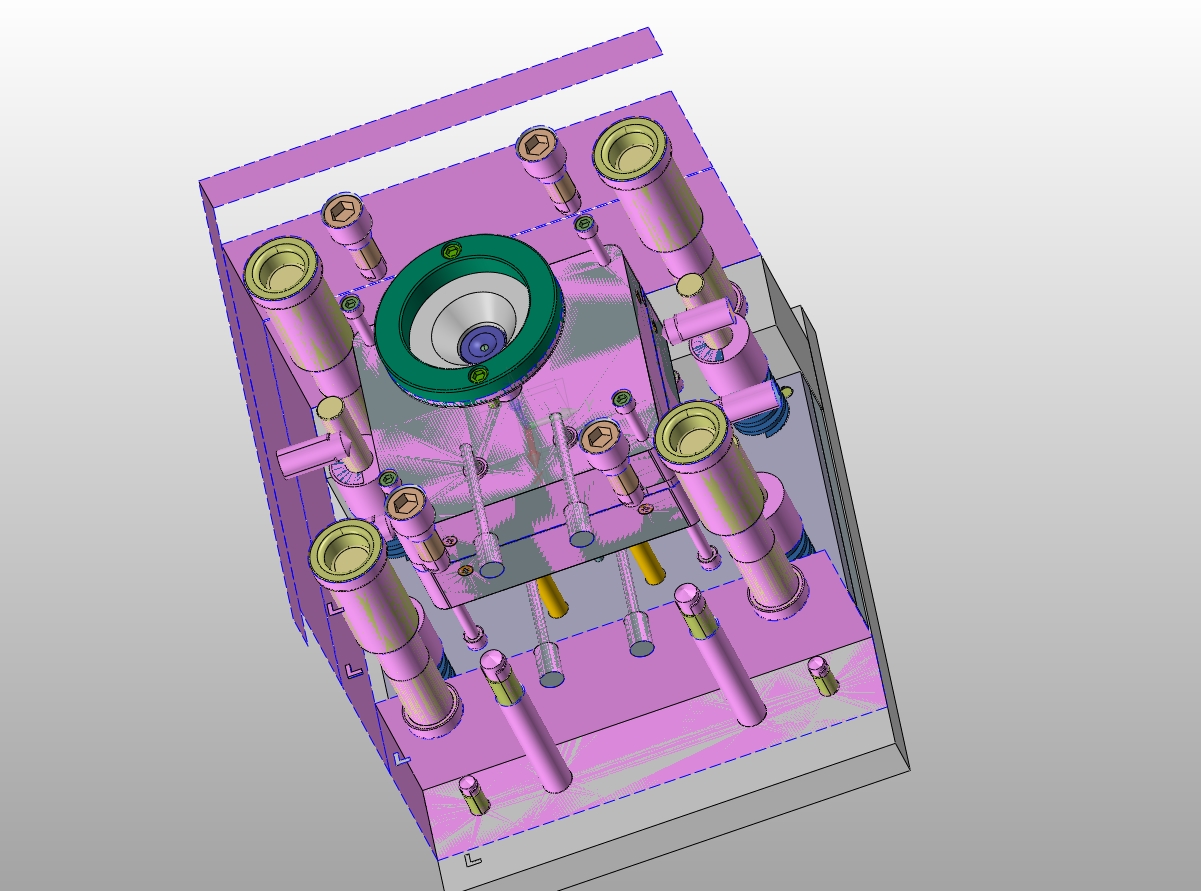
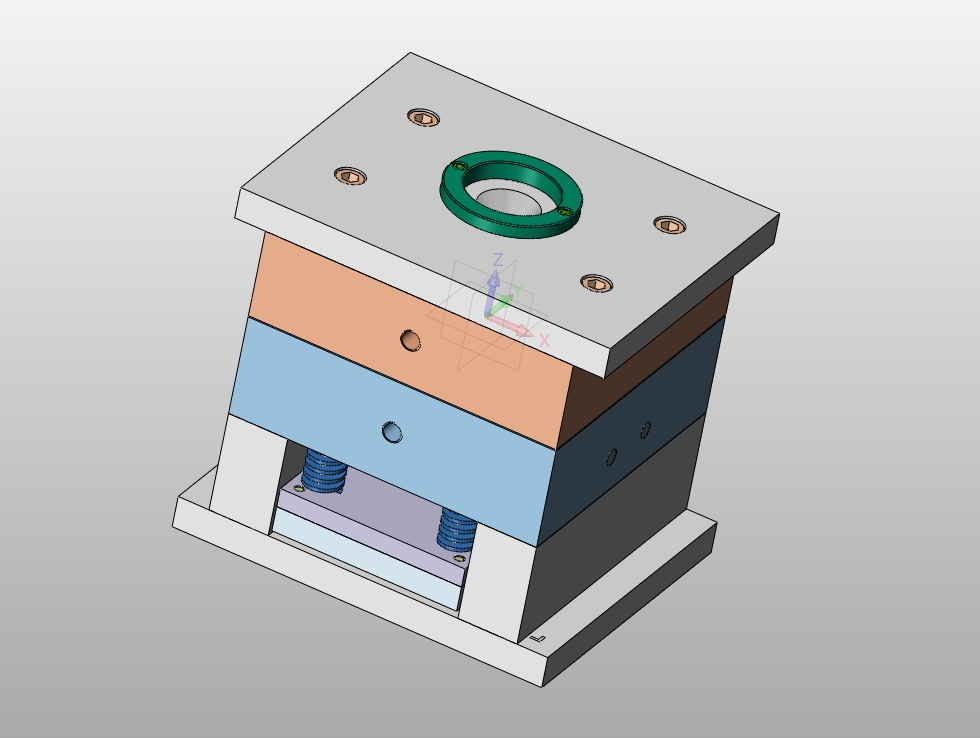
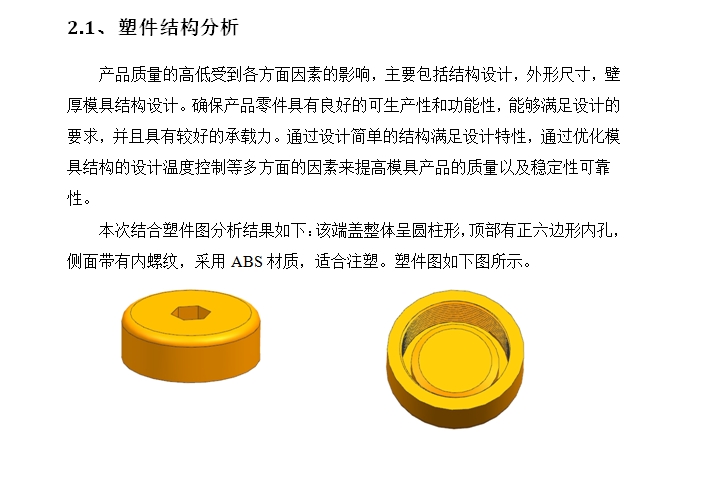
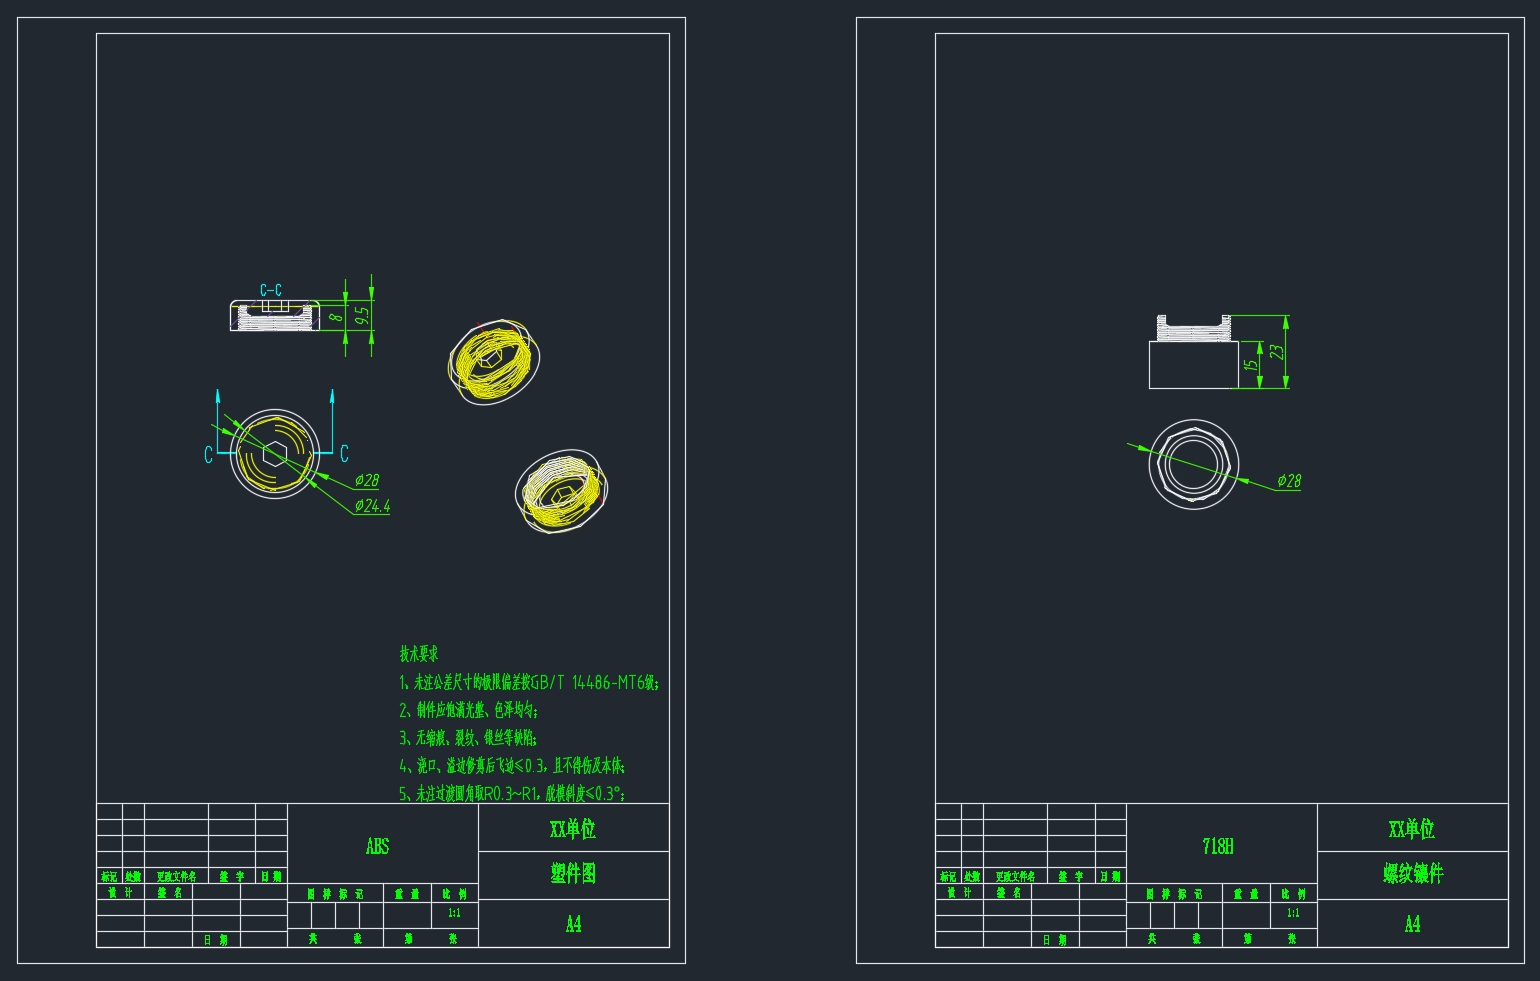
端盖是我们日常生活常见的塑件产品,通过查阅相关的资料和数据,根据塑料材料的特性选用高分子热塑性材料中的ABS材料,在生产加工过程中能够提高生产的质量以及塑料的稳定性。并且根据端盖的结构尺寸以及相关要求确定注塑的工艺。其主要成型零部件采用了型芯型腔镶嵌式。浇注系统通过侧浇口进行注塑充填,再通过环绕式冷却水道冷却系统和顶杆顶出脱模完成端盖产品的生产和加工。在生产加工过程中要严格的按照零件图的图纸要求对模具结构进行设计,并且要满足实际的生产加工。
通过该端盖的注塑模具结构的研究和设计,能够推动模具行业的发展,降低生产加工的成本,提高经济效益。
关键词:注塑模具设计;高分子材料;模具结构;成型;工艺;
Abstract
With the continuous improvement of economic level and the continuous development of society, it has also promoted the progress of the machinery industry. With the continuous improvement of people's living standards, various plastic products are used in daily life. This article mainly focuses on the design of injection molds for end caps, using plastic molding technology to produce and process them, and designing an efficient and economical mold structure. [版权所有:http://DOC163.com]
End caps are common plastic products in our daily lives. By consulting relevant information and data, ABS material from polymer thermoplastic materials is selected based on the characteristics of plastic materials. This can improve the quality of production and the stability of plastics during the production and processing process. And determine the injection molding process based on the structural dimensions and relevant requirements of the end cap. Its main molded components adopt a core cavity inlay type. The pouring system is filled with injection molding through side gates, and then the production and processing of end cap products are completed through a surrounding cooling water channel cooling system and top rod ejection demolding. During the production and processing process, it is necessary to strictly design the mold structure according to the requirements of the part drawing and meet the actual production and processing needs.
The research and design of the injection mold structure for this end cap can promote the development of the mold industry, reduce production and processing costs, and improve economic benefits.
Keywords: Injection mold design; Polymer materials; Mold structure; forming; workmanship
塑料材料的选用
目前社会上有各种不同类型不同结构和不同材料的塑料产品。在设计过程中要对结构特性,加工性能材料特性等多方面综合考虑。尽可能的保证所选用的材料具有良好的特性,具有良好的耐腐蚀性、绝缘性。与金属材料相比较材料的密度较低。主要是生产一些质量较轻的零件,并且具有较好的耐腐蚀性和延展性,被广泛地应用在电子产品领域内[15]。
本文所设计的端盖根据使用的特点和要求选择ABS材料,其主要性能如下表所示。
表2-1 材料主要性能参数
具体性能 参数数值
拉伸强度 50 - 75 MPa
断裂伸长率 30% - 250%
弯曲强度 80 - 120 MPa
弯曲模量 2000 - 4000 MPa
冲击强度(缺口) 4 - 15 kJ/m²
熔点 250 - 260 °C
玻璃化转变温度 70 - 80 °C
热变形温度(1.82MPa) 60 - 85 °C
线膨胀系数 (1.8 - 3.0)×10⁻⁵ /°C [资料来源:http://www.doc163.com]
密度 1.07 g/cm³
吸水率(24h) 0.1% - 0.2%
材料收缩率 0.06-0.08
材料允许的注射压力 50-100(中高)Mpa
表面电阻率 ≥10¹³ Ω
介电常数(1MHz) 3.0 - 3.8
介电损耗因数(1MHz) ≤0.01
耐酸性能 良好
耐碱性能 一般,在高温高浓度碱液中会水解
耐有机溶剂性能 良好,对烃类、醇类、酯类等有较好耐受性 -
 [版权所有:http://DOC163.com]
目录
摘要 I
Abstract II
目录 III
第一章、引言 1
1.1、塑料模具的概述 1
1.2、国内塑料模具产业发展现状 1
1.3、国外模具产业发展现状 2
1.5、塑料模具毕业设计的意义 4
第二章、塑件工艺结构分析 5
2.1、塑件结构分析 5
2.2、塑料材料的选用 6
2.3、注塑成型工艺拟定 7
2.4、注塑生产的工艺流程 8
第三章、确定设计方案与注塑机的选择 10
3.1、分型面的选择 10
3.2、型腔数量的确定 10
3.3、选择模架类型 11
3.4、计算注射量 12
3.5、选择注塑机 13
第四章、浇注系统设计 15
4.1、浇注系统的概述 15
4.2、主流道的设计 15 [资料来源:http://doc163.com]
4.3、分流道的设计 18
4.4、浇口的设计 20
4.5、冷料穴的设计 22
4.6、模具排气 23
第五章、成型零部件结构设计 24
5.1、成型系统的概述 24
5.2、型腔结构设计 24
5.3、型芯结构设计 25
5.4、成型尺寸的计算 25
5.4.1、塑件型腔成型尺寸计算 25
5.4.2、塑件型芯成型尺寸计算 27
5.5、成型零件侧壁底壁强度校核 28
5.6、成型零件钢材选用 29
第六章、注塑模具其余机构设计 31
6.1、冷却系统 31
6.1.1、冷却系统计算 31
6.1.2、冷却水道的设计 34
6.2、推出脱模机构 35
6.2.1、脱模结构计算与校核 35
6.2.2、推出脱模机构设计 37
6.3、复位杆结构设计 37 [资料来源:https://www.doc163.com]
6.4、导向机构设计 38
6.5、注塑机的概述 38
6.6、注塑机参数校核 38
附图 41
总结 42
致谢 43
参考文献 44 [来源:http://Doc163.com]